
PENTAIR X-FLOW PLUG & PLAY SKID MOUNTED UNITS
PENTAIR X-FLOW PLUG & PLAY SKID MOUNTED UNITS
Pentair’s packaged Plug & Play units come in the perfect configuration to suit a variety of applications, from potable water production to the treatment of process and wastewater and the pre-treatment of seawater, but also for the food, beverage and pharmaceutical industries. We can help you pick the best preconfigured unit for your needs, and assemble it for you, delivered anywhere in Africa!

AIRLIFT
Pentair X-Flow Airlift Solution delivers a cost-effective membrane bioreactor (MBR) solution for municipal and industrial wastewater treatment applications. The X-Flow Airlift solution eliminates the build-up of debris at the membrane inlet with the drain step.
Airlift uniquely combines membranes with biological treatment. Another major advantage of the Airlift technology is that the membrane modules are placed outside the bioreactor in a clean and dry setup. The wastewater itself is inside the membranes rather than outside, thus eliminating the problem of maintaining modules submerged in activated sludge. The membranes are easily accessible and cleaned.
For capacities >7,5 MLD the application of our Airlift Megablock can be of interest.
AQUAFLEX
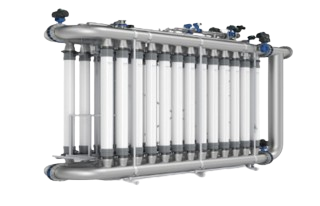
Pentair X-Flow Aquaflex Solution is the ideal Ultrafiltration Solution for challenging feed waters. It helps address challenging surface water, groundwater, seawater, and wastewater treatment requirements.
Features
- Broad skid range: 10-120 membrane elements
- Handling of feedwaters up to 250 mg/l total suspended solids (TSS) or 100 NTU turbidity
- Vertical dead-end can be applied in a broad range of applications, from industrial to drinking water production
Pentair X-Flow Aquaflex High Solids (HS) Solution eliminates the need for conventional pre-treatment requirements of traditional ultrafiltration (UF) systems. This reduces overall cost of ownership, with a one-step high solids filtration, and is perfect for wastewater treatment, when suspended matter is above 200 ppm.

CROSSFLOW MBR
Developed for (industrial) wastewater applications, the X-Flow Crossflow MBR Solution is at its best with difficult to treat wastewater. It combines membranes with biological treatment.
Crossflow MBR needs more energy (1,5-4 kWh/m³) than our X-Flow Airlift Solution (<0,25 kWh/m3), but offers the advantages of a continuous process and a minimal footprint. Furthermore, it can deal with very high MLSS (12-30+ g/l) and work with a significantly higher flux (80-200 l/m2h).

CROSSFLOW UF
The Pentair X-Flow Crossflow UF Solution operates based on turbulence, using the Pentair X-Flow 5.2 or 8 mm Compact Tubular Membrane Elements. Benefitting from the Pentair X-Flow Helix Technology, it prevents cake formation on the membrane layer.
The robustly designed X-Flow Crossflow UF Solution is available in four sizes: 1×8 modules, 2×8 membrane elements, 3×8 membrane elements and 4×8 membrane elements, with performances ranging respectively from approximately 50 to 100, 150 and 250 m3/h.
For capacities under 50 m3/h the X-Flow Crossflow MBR Solution can be considered.

HF NANO
Pure and clean water from surface water without the use of chemicals! Install Pentair X-Flow HFNANO with the Pentair X-Flow HFW1000 membrane elements, it leverages the strengths of hollow fibre technology and nanofiltration (NF) membranes into a sustainable membrane filtration solution.
The X-Flow HFNANO Solution eliminates the need for coagulants to remove dissolved organics from difficult surface water sources. It uniquely removes color and organics from drinking water and wastewater and can be used in both municipal and industrial operations.
REVERTA
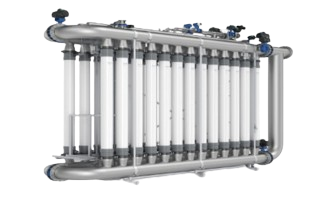
Designed for AnMBR wastewater treatment, X-Flow Reverta reverses the feed flow, which prevents cake formation on the membrane layer while producing higher permeate flows at lower cross-flow velocities. With X-Flow Reverta you can rely on consistent delivery of high-quality effluent while producing the maximum amount of biogas, all with minimal operator interference.
When do you choose AnMBR to treat wastewater?
- Water is very high in organic content. Concentrations of COD >7,000 ppm
- Total amount of COD >3,000 kg/day
- High salinity
- High FOG levels without DAF being applied (up to ca 1,000 ppm)
- Food & Beverage industry
- (Bio)ethanol production: pot ale, spent wash, thin stillage and vinasse
- FOG in waste streams from ice cream, candy, and biodiesel production
- Starch slurries

X-FLLOW NANOQUBE
X-Flow Nanoqube utilises the uniquely designed Pentair X-Flow Hollow Fibre HFW1000 Hydrophilic Nanofiltration Membrane Elements. It is specifically designed to help meet the drinking water requirements of small communities and facilities. Net capacity ranges from 1.5 to 10 m3/hr, depending on system size and feed water quality.
Benefits
- No need for membrane housings and headers
- Reduced design capacity of circulation pump
- Flow velocity in end-cap connections is sufficiently high to help avoid accumulation of solids/and fouling
- Optimum compact overall design, a fully functional system fits inside a standard shipping container
- High removal of dissolved organic matter (NOM, DOC, UV254),turbidity and suspended solids
- Certified for bacteria and viruses
- Minimum removal of hardness and salts (Mg, Ca)
- High cleanability
- Stable long-term performance
- No special pre-treatment being required other than a 200 micron strainer
X-LINE
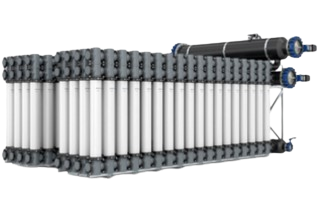
The X-line Rack is a revolutionary, pre-engineered ultrafiltration (UF) solution. This unique concept creates maximum flexibility in rack design and a minimised footprint.
Due to its dead-end operation with hydraulic cleaning and chemically enhanced backwashes, the versatile X-line rack is suitable for a wide range of industrial and municipal applications. A steady and well-distributed flow means better and consistent performance during the entire lifecycle, and an optimal footprint-to-flow ratio.
X-flow is available in various rack configurations, please contact us for more information
XIGA
Xiga is the Ideal solution for large-scale ultrafiltration applications in a small footprint. With the highest membrane area-to-footprint ratio in the market, Xiga is developed for the treatment of surface water (to produce potable water or process water) and drinking water. It it also applicable for wastewater polishing and reuse, and as a pre-treatment step for seawater RO.
- Up to four membrane elements can be placed in one GRP housing
- Operating pressure up to 8 barg
- Suitable for inline operation
- High reference base, used in multiple large ultrafiltration (UF) plants around the world
- Direct filtration of all water sources
Pentair’s packaged Plug & Play units come in the perfect configuration to suit a variety of applications, from potable water production to the treatment of process and wastewater and the pre-treatment of seawater, but also for the food, beverage and pharmaceutical industries. We can help you pick the best preconfigured unit for your needs, and assemble it for you, delivered anywhere in Africa!
AIRLIFT
Pentair X-Flow Airlift Solution delivers a cost-effective membrane bioreactor (MBR) solution for municipal and industrial wastewater treatment applications. The X-Flow Airlift solution eliminates the build-up of debris at the membrane inlet with the drain step.
Airlift uniquely combines membranes with biological treatment. Another major advantage of the Airlift technology is that the membrane modules are placed outside the bioreactor in a clean and dry setup. The wastewater itself is inside the membranes rather than outside, thus eliminating the problem of maintaining modules submerged in activated sludge. The membranes are easily accessible and cleaned.
For capacities >7,5 MLD the application of our Airlift Megablock can be of interest.
AQUAFLEX
Pentair X-Flow Aquaflex Solution is the ideal Ultrafiltration Solution for challenging feed waters. It helps address challenging surface water, groundwater, seawater, and wastewater treatment requirements.
Features
- Broad skid range: 10-120 membrane elements
- Handling of feedwaters up to 250 mg/l total suspended solids (TSS) or 100 NTU turbidity
- Vertical dead-end can be applied in a broad range of applications, from industrial to drinking water production
Pentair X-Flow Aquaflex High Solids (HS) Solution eliminates the need for conventional pre-treatment requirements of traditional ultrafiltration (UF) systems. This reduces overall cost of ownership, with a one-step high solids filtration, and is perfect for wastewater treatment, when suspended matter is above 200 ppm.
CROSSFLOW MBR
Developed for (industrial) wastewater applications, the X-Flow Crossflow MBR Solution is at its best with difficult to treat wastewater. It combines membranes with biological treatment.
Crossflow MBR needs more energy (1,5-4 kWh/m³) than our X-Flow Airlift Solution (<0,25 kWh/m3), but offers the advantages of a continuous process and a minimal footprint. Furthermore, it can deal with very high MLSS (12-30+ g/l) and work with a significantly higher flux (80-200 l/m2h).
CROSSFLOW UF
The Pentair X-Flow Crossflow UF Solution operates based on turbulence, using the Pentair X-Flow 5.2 or 8 mm Compact Tubular Membrane Elements. Benefitting from the Pentair X-Flow Helix Technology, it prevents cake formation on the membrane layer.
The robustly designed X-Flow Crossflow UF Solution is available in four sizes: 1×8 modules, 2×8 membrane elements, 3×8 membrane elements and 4×8 membrane elements, with performances ranging respectively from approximately 50 to 100, 150 and 250 m3/h.
For capacities under 50 m3/h the X-Flow Crossflow MBR Solution can be considered.
HF NANO
Pure and clean water from surface water without the use of chemicals! Install Pentair X-Flow HFNANO with the Pentair X-Flow HFW1000 membrane elements, it leverages the strengths of hollow fibre technology and nanofiltration (NF) membranes into a sustainable membrane filtration solution.
The X-Flow HFNANO Solution eliminates the need for coagulants to remove dissolved organics from difficult surface water sources. It uniquely removes color and organics from drinking water and wastewater and can be used in both municipal and industrial operations.
REVERTA
Designed for AnMBR wastewater treatment, X-Flow Reverta reverses the feed flow, which prevents cake formation on the membrane layer while producing higher permeate flows at lower cross-flow velocities. With X-Flow Reverta you can rely on consistent delivery of high-quality effluent while producing the maximum amount of biogas, all with minimal operator interference.
When do you choose AnMBR to treat wastewater?
- Water is very high in organic content. Concentrations of COD >7,000 ppm
- Total amount of COD >3,000 kg/day
- High salinity
- High FOG levels without DAF being applied (up to ca 1,000 ppm)
- Food & Beverage industry
- (Bio)ethanol production: pot ale, spent wash, thin stillage and vinasse
- FOG in waste streams from ice cream, candy, and biodiesel production
- Starch slurries
X-FLLOW NANOQUBE
X-Flow Nanoqube utilises the uniquely designed Pentair X-Flow Hollow Fibre HFW1000 Hydrophilic Nanofiltration Membrane Elements. It is specifically designed to help meet the drinking water requirements of small communities and facilities. Net capacity ranges from 1.5 to 10 m3/hr, depending on system size and feed water quality.
Benefits
- No need for membrane housings and headers
- Reduced design capacity of circulation pump
- Flow velocity in end-cap connections is sufficiently high to help avoid accumulation of solids/and fouling
- Optimum compact overall design, a fully functional system fits inside a standard shipping container
- High removal of dissolved organic matter (NOM, DOC, UV254),turbidity and suspended solids
- Certified for bacteria and viruses
- Minimum removal of hardness and salts (Mg, Ca)
- High cleanability
- Stable long-term performance
- No special pre-treatment being required other than a 200 micron strainer
X-LINE
The X-line Rack is a revolutionary, pre-engineered ultrafiltration (UF) solution. This unique concept creates maximum flexibility in rack design and a minimised footprint.
Due to its dead-end operation with hydraulic cleaning and chemically enhanced backwashes, the versatile X-line rack is suitable for a wide range of industrial and municipal applications. A steady and well-distributed flow means better and consistent performance during the entire lifecycle, and an optimal footprint-to-flow ratio.
X-flow is available in various rack configurations, please contact us for more information
XIGA
Xiga is the Ideal solution for large-scale ultrafiltration applications in a small footprint. With the highest membrane area-to-footprint ratio in the market, Xiga is developed for the treatment of surface water (to produce potable water or process water) and drinking water. It it also applicable for wastewater polishing and reuse, and as a pre-treatment step for seawater RO.
- Up to four membrane elements can be placed in one GRP housing
- Operating pressure up to 8 barg
- Suitable for inline operation
- High reference base, used in multiple large ultrafiltration (UF) plants around the world
- Direct filtration of all water sources